Wire Harness Electrical Testing: Continuity, Hi-Pot and Contact Resistance Explained
Wire Harness Electrical Testing: Continuity, Hi-Pot and Contact Resistance Explained
Define the harness architecture and verification plan before comparing an assembly approach. Use the controlled drawing, actual operating conditions, and approval requirements.
Inhalt
What should an electrical test plan prove?
A harness test plan should prove the specific conditions named in the controlled drawing and acceptance plan. It is not a generic list of instruments; continuity, insulation, dielectric checks, and contact resistance each answer different questions. For a related technical reference, see Wire Harness Branch Design: Choosing Splices, Junctions and Breakouts.
| Review area |
Buyer needs to define |
Why it matters |
| Controlled configuration |
Drawing, interface, and operating condition |
Prevents a generic answer from becoming a release decision |
| Mechanical architecture |
Routing, protection, fixture, and service constraints |
Reveals physical conflicts early |
| Acceptance evidence |
Samples, methods, limits, and records |
Makes supplier and engineering reviews comparable |
How does continuity testing fit the sequence?
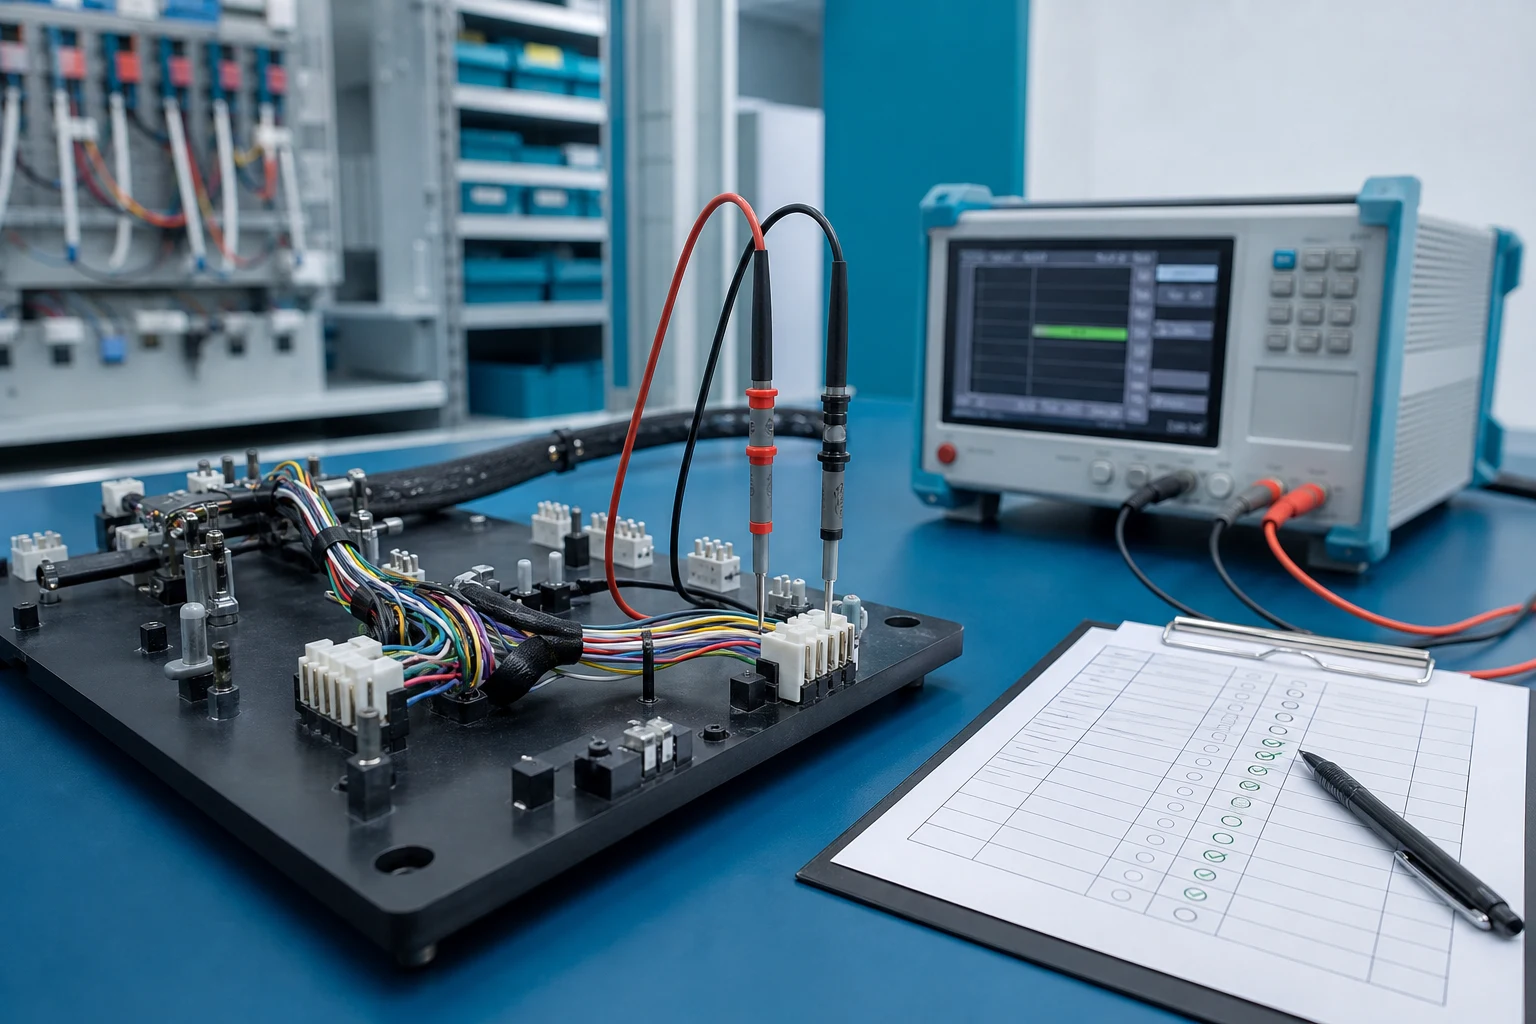
Continuity verifies intended circuit paths and can identify opens, swaps, and selected shorts when the fixture and pin map are correct. Define the connector state, test points, circuit list, acceptance criteria, and handling of intermittent results.
When is hi-pot or insulation testing relevant?
High-potential or insulation-resistance testing may be relevant only when the application, drawing, and governing requirements call for it. Define voltage, duration, safety controls, and acceptance limits in the approved plan rather than copying a generic setting.
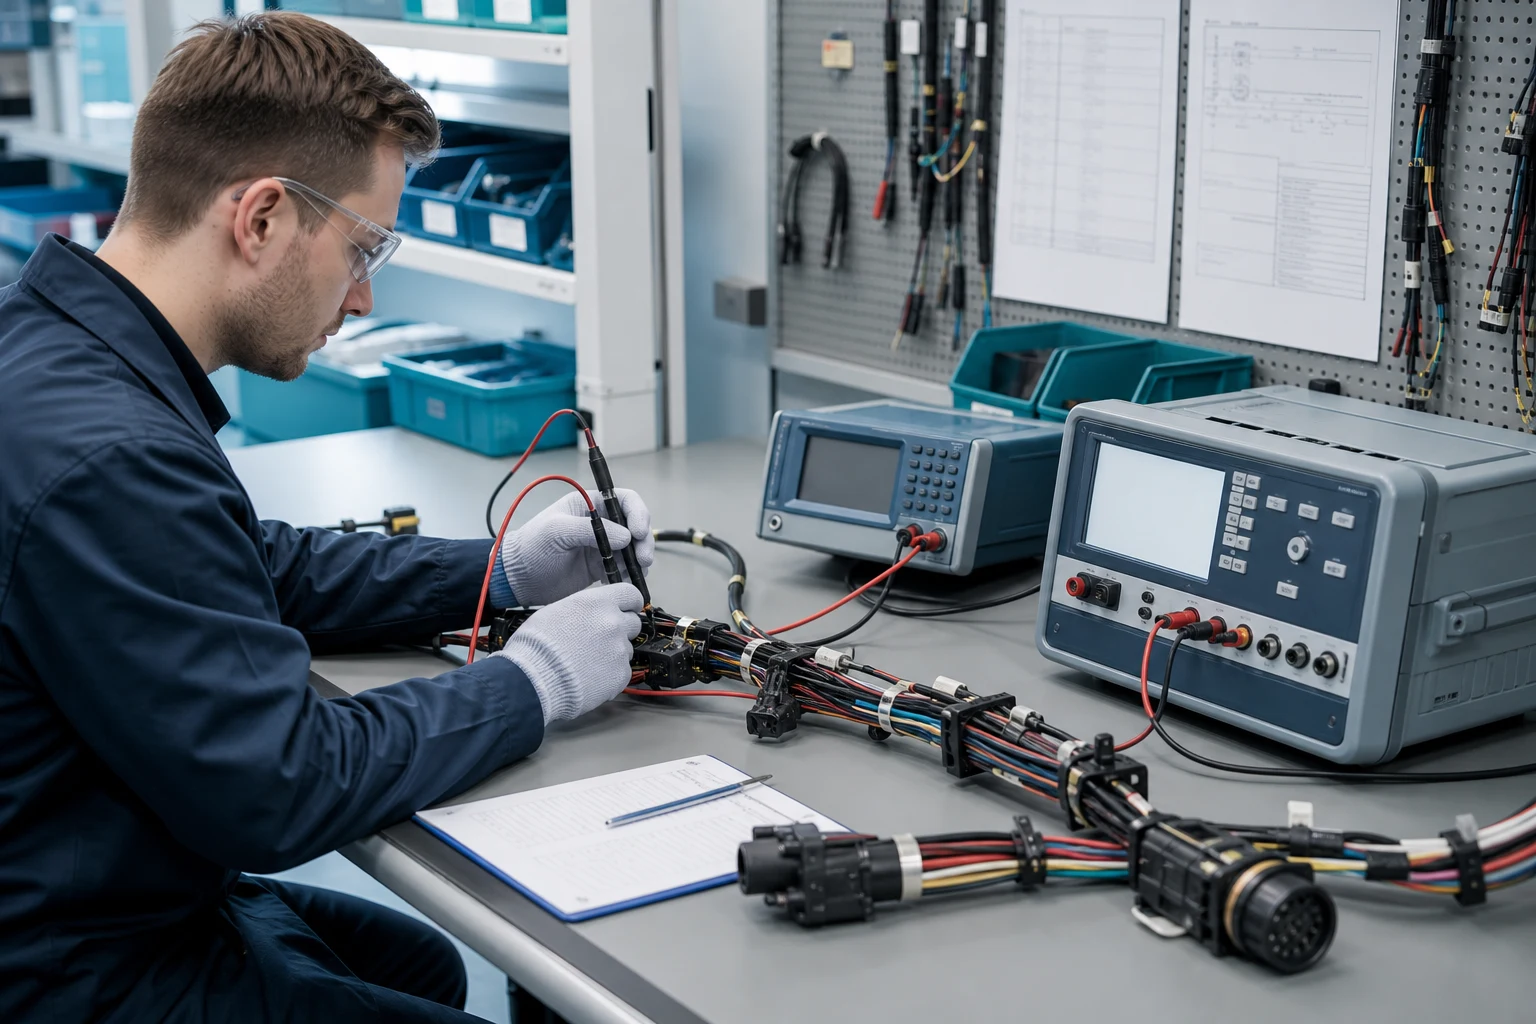
Contact-resistance measurement can help evaluate a defined interface when the method, current, measurement points, conditioning, and limits match the application. It does not replace a broader system validation.
How should fixtures and test access be controlled?
The fixture must represent the correct mating interfaces and avoid damaging the part. Control pin maps, probe condition, calibration, software version, test sequence, sample identification, and retest logic. For a related technical reference, see Male Tab Terminals: How Tab Width and Thickness Affect Mating Performance.
Wichtig: General guidance cannot approve a finished harness. This is a source-note application of the IPC and TE references below; use the controlled drawing and programme acceptance plan.
What records support release?
Retain the defined result, unit or lot identity, test configuration, operator or system record, nonconformance route, and approved disposition. Define changes that require fixture or test-plan review.
Which ZUCH route supports a controlled inquiry?
Use ZUCH’s ZUCH innovation route and the live product catalogue to identify relevant connector or terminal component families. These are discovery routes only and do not demonstrate a finished harness is approved.
RFQ inputs
- Controlled drawing, revision, interface, and circuit definition.
- Routing, environment, service, and mechanical constraints.
- Required samples, inspection/tests, acceptance criteria, and records.
- Change-control and nonconformance expectations.
Fit Boundary
This guide supports engineering and sourcing discussion; it cannot replace programme-specific validation, market requirements, or an approval record. Use ZUCH’s sample request route or contact page for controlled component documentation and samples.
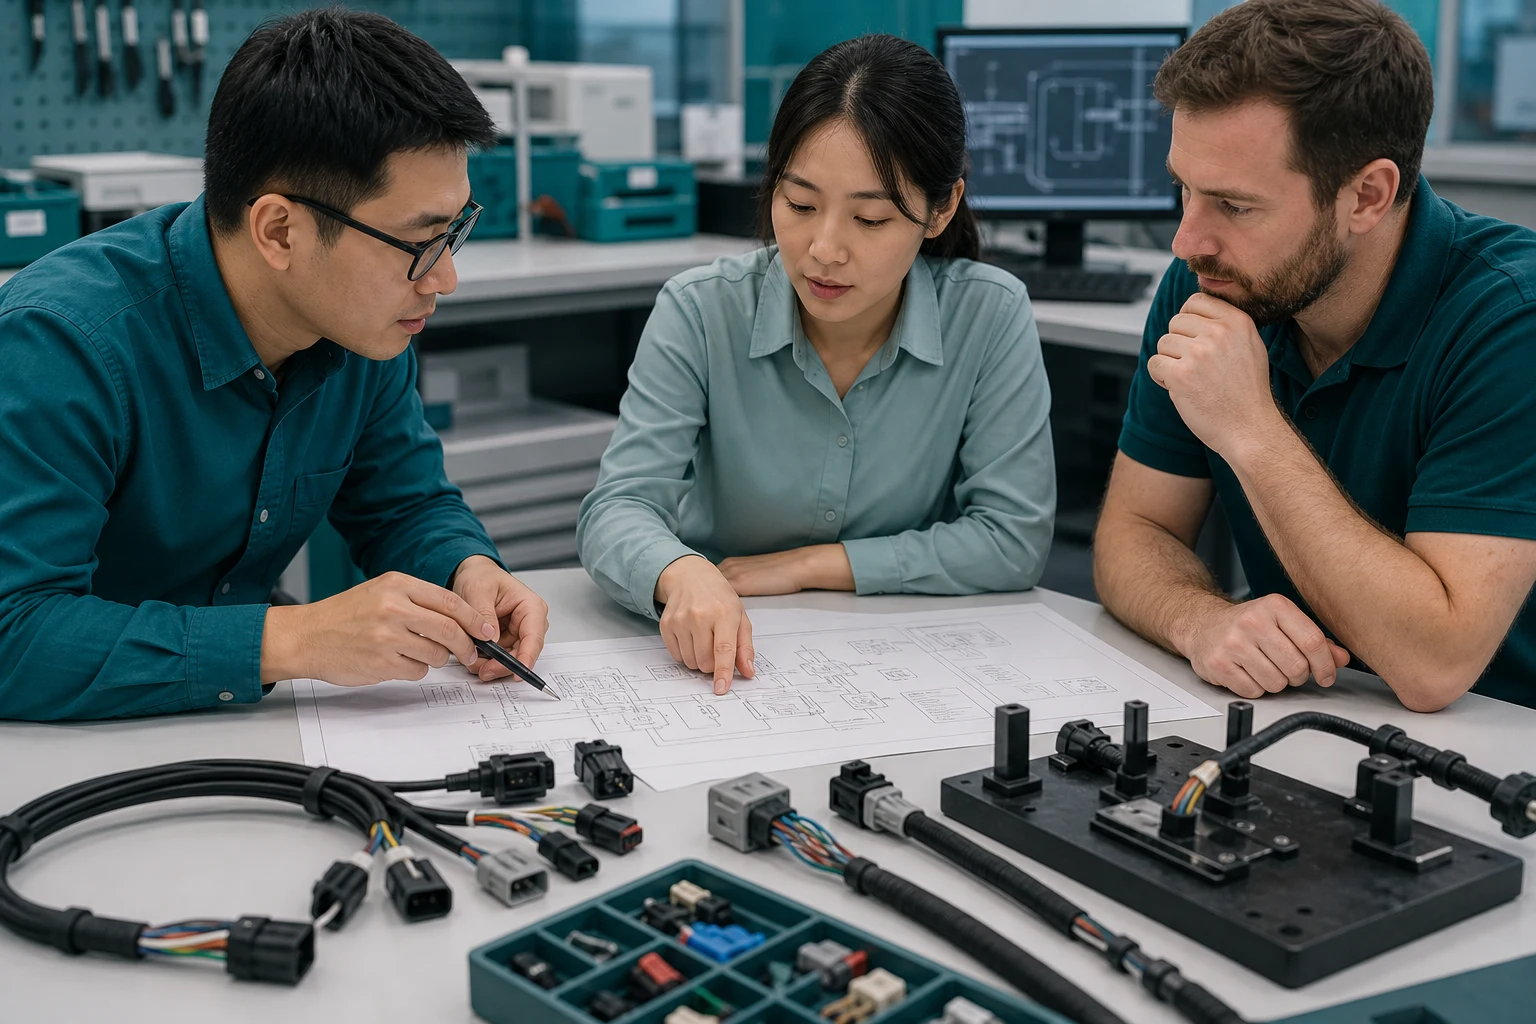
Sequence harness tests from wiring identity to electrical acceptance
A useful harness test plan separates what each test proves. Continuity and point-to-point checks verify wiring identity; insulation or hi-pot testing addresses a defined dielectric requirement; contact-resistance testing examines the connection path under its stated method. None of these tests alone proves long-term mechanical durability.
| Test layer |
What it can establish |
What it cannot establish by itself |
| Continuity / point-to-point |
Expected circuits are connected and unintended opens are found |
Long-term wear, sealing, vibration durability, or every intermittent fault |
| Insulation / hi-pot where applicable |
The specified dielectric or insulation condition under the defined method |
A universal requirement for every harness or proof of connector life |
| Contact resistance |
Connection-path resistance under the defined current, probes and condition |
Correct pinout, mechanical retention, or system-level thermal performance |
| Functional test |
The assembly operates in the intended equipment or test setup |
A substitute for a controlled drawing, process record, or lot traceability |
FAQ
Is hi-pot required for every wire harness?
No. The requirement depends on the circuit, insulation system, product standard, customer specification, and risk. Define the method and limit from the applicable requirement instead of applying a generic voltage.
What does contact-resistance testing add?
It evaluates the connection path under a defined test setup and can reveal issues that a simple continuity check will not quantify. The method, probe points, current and limit must remain part-specific.
Why does the test fixture matter?
Fixture pinout, contact condition, force, access and software logic can create false passes or failures. Keep the fixture revision-controlled and verify it against a known-good assembly or reference.
Can continuity testing prove long-term durability?
No. Continuity is a wiring check at the time of test. Durability requires separate mechanical, environmental, mating, vibration or lifecycle evidence where the program needs it.
What is wire harness continuity testing?
It checks whether the intended electrical path is complete and correctly mapped under the controlled test configuration.
Is hi-pot required for every harness?
No. Use it only when the application, drawing, and applicable requirements define that test and its conditions.
What does contact resistance testing show?
It measures a defined electrical interface under a controlled method; its value depends on the configuration, current, points, and acceptance limits.
Why does the test fixture matter?
A wrong pin map, worn probe, or incorrect mating interface can produce misleading results or damage the harness.
What should a harness test record contain?
Include the unit or lot identity, test setup, sequence, results, acceptance status, and nonconformance disposition required by the program.
Can a continuity test prove long-term durability?
No. It confirms the defined electrical path at the test condition; environmental and mechanical durability require their own agreed evaluation.
What should buyers include in a harness test RFQ?
Include the drawing, circuit map, required tests and limits, fixture/interface inputs, sample plan, records, safety requirements, and change-control expectations.
Key takeaway
A harness test plan is stronger when every test has one stated purpose, one method, one acceptance boundary, and one retained record. Sequence tests from identity to electrical condition, then use separate evidence for mechanical and environmental risks.
References
 Zhejiang ZUCH Technology Co., Ltd.